Oct . 13, 2025 14:25 Back to list
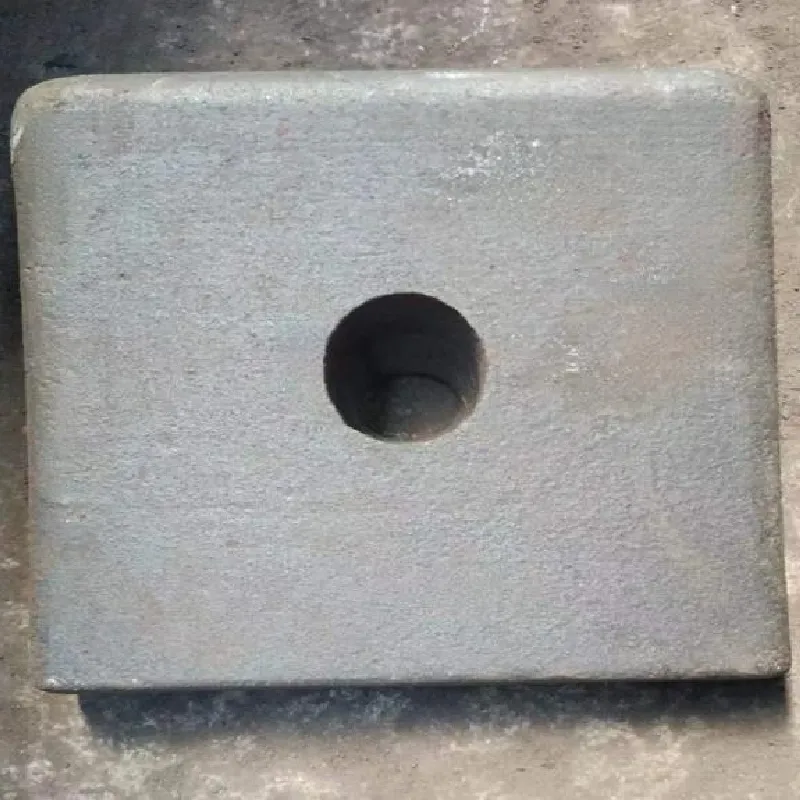
Chromium Carbide Liner – Ultra Wear-Resistant, Long Life
Field Notes on the Chromium Carbide Liner Trend (and Why High-Chromium Alloy Still Wins)
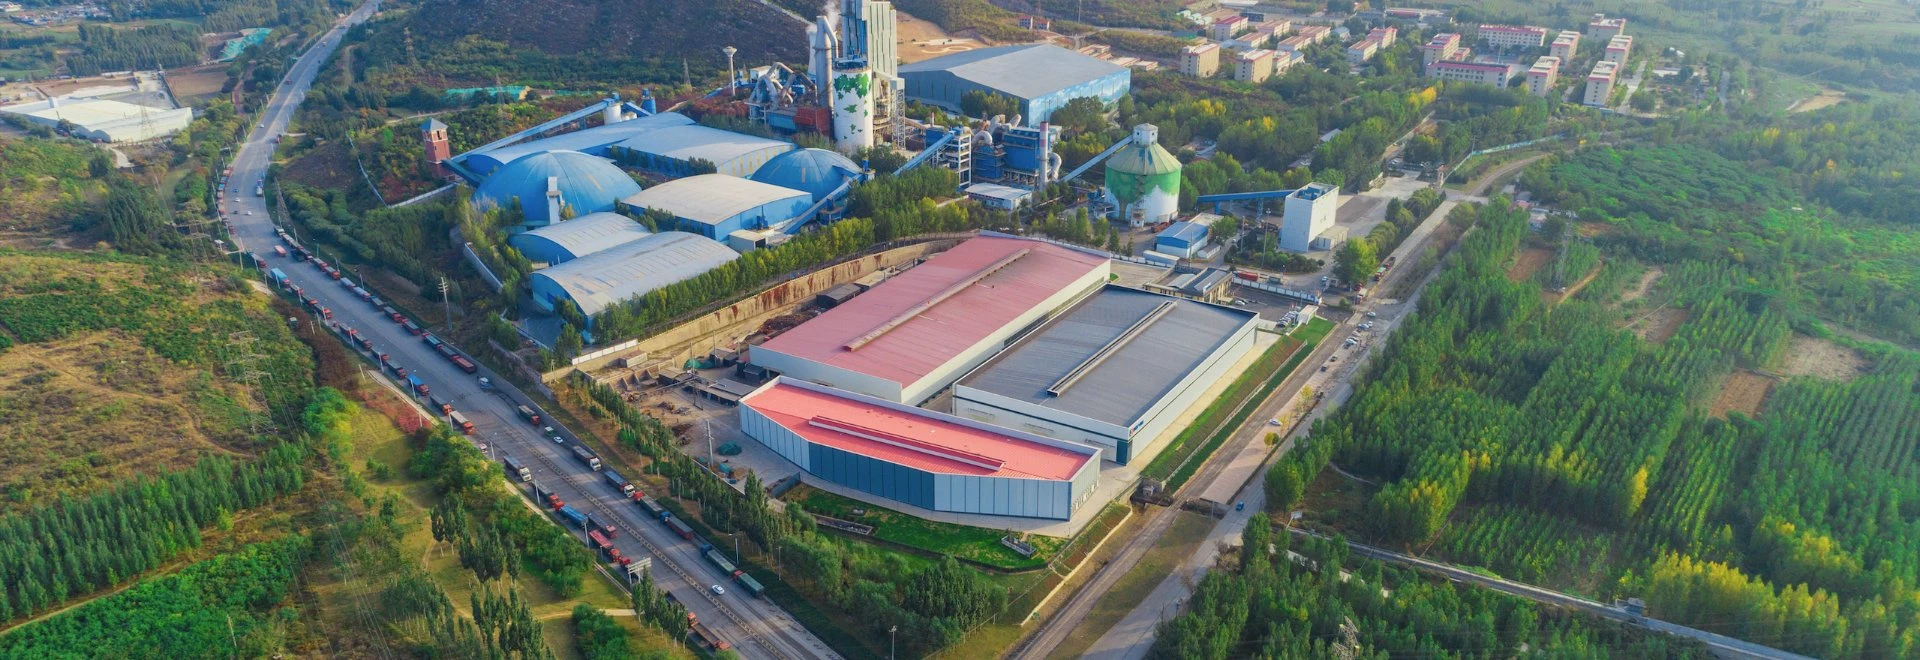
If you’ve spent time in a quarry chute or a clinker line (I have, boots and all), you know wear parts make or break uptime. So when people ask about a chromium carbide liner, I usually say: yes—great choice for abrasion—but don’t overlook cast high-chromium alloy liners from Hebei, China. Chengda’s foundry in KIZUN Industry Zone, Luquan, Shijiazhuang, has been turning out tough parts that actually hold up in dirty, real-world conditions.
What’s moving the market
Two currents: cost-per-ton scrutiny and maintenance constraints. Plants in mining, cement, aggregates, and power are shifting from AR plate to high-chrome or chromium carbide liner solutions because the service life jump (2–5×, sometimes more) is hard to ignore. Actually, sustainability is part of it too—fewer changeouts means lower waste and safer crews.
How Chengda builds durability
-
- Materials: High-chromium white iron (ASTM A532 Class III, Type A), engineered for Cr-rich M7C3 carbides.
- Methods: Controlled melt, precision casting (lost foam/sand), heat treatment (austempering/tempering) for carbide stability.
- QA/Testing: Hardness mapping (Rockwell per ISO 6508-1), Brinell checks (ISO 6506-1), UT/MT for integrity, abrasion benchmarking (ASTM G65).
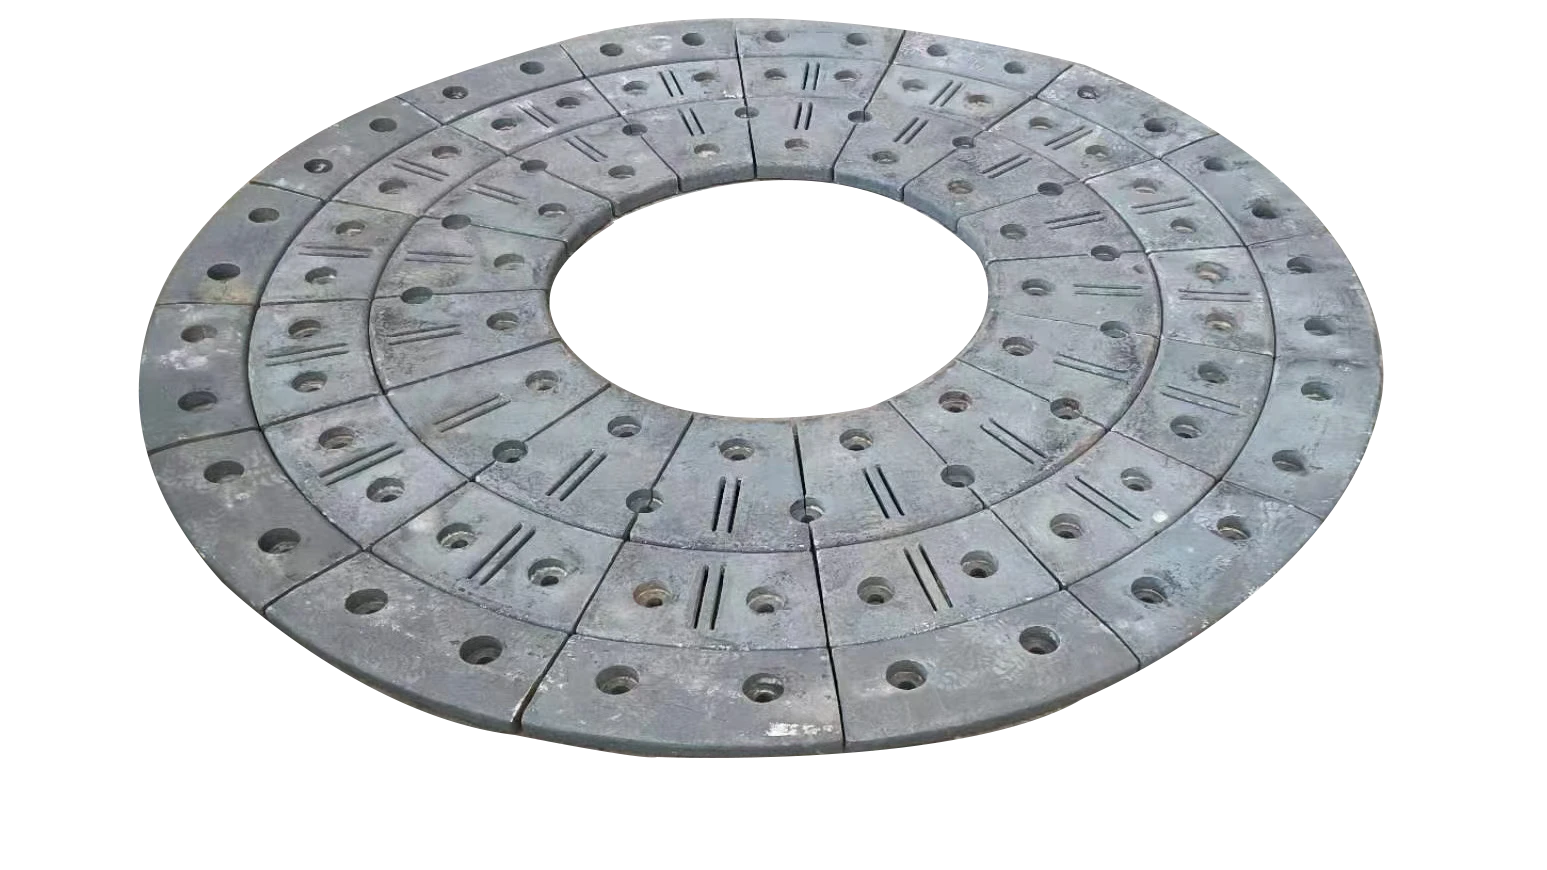
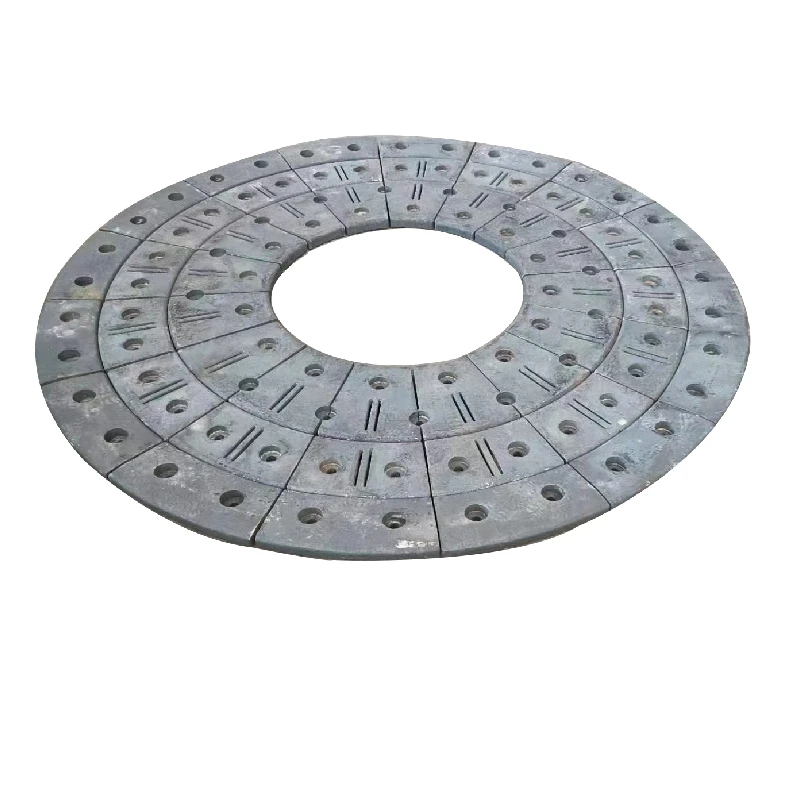
- Finishing: CNC drilling, countersinks, studs; flat or curved segments; bimetal options with mild-steel backing.
- Certifications: ISO 9001:2015 quality management, mill test reports per heat.
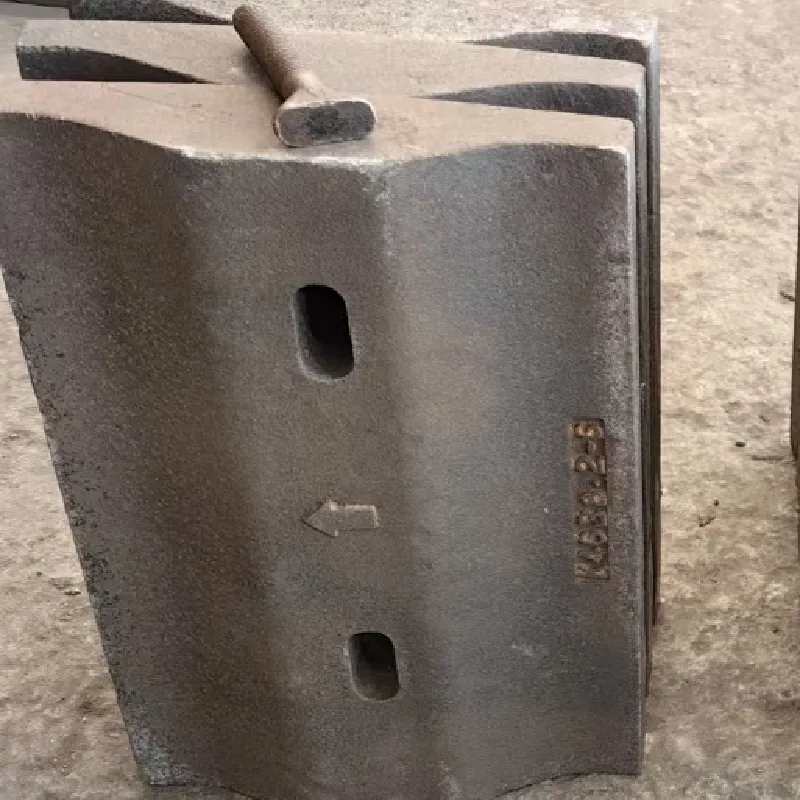
Product snapshot: High chromium alloy liner
| Material standard | ASTM A532 Cl. III (≈20–28% Cr) |
| Hardness | HRC 60–64 (ISO 6508-1; real-world use may vary) |
| Carbide volume fraction | ≈ 30–45% |
| ASTM G65 (Proc A) | Mass loss ≈ 0.10–0.18 g |
| Impact tolerance | Around 5–8 J (design- and thickness-dependent) |
| Service life vs. AR400 | ≈ 2–5× (media, angle, and fines content matter) |
| Typical thickness | 12–50 mm cast; custom on request |
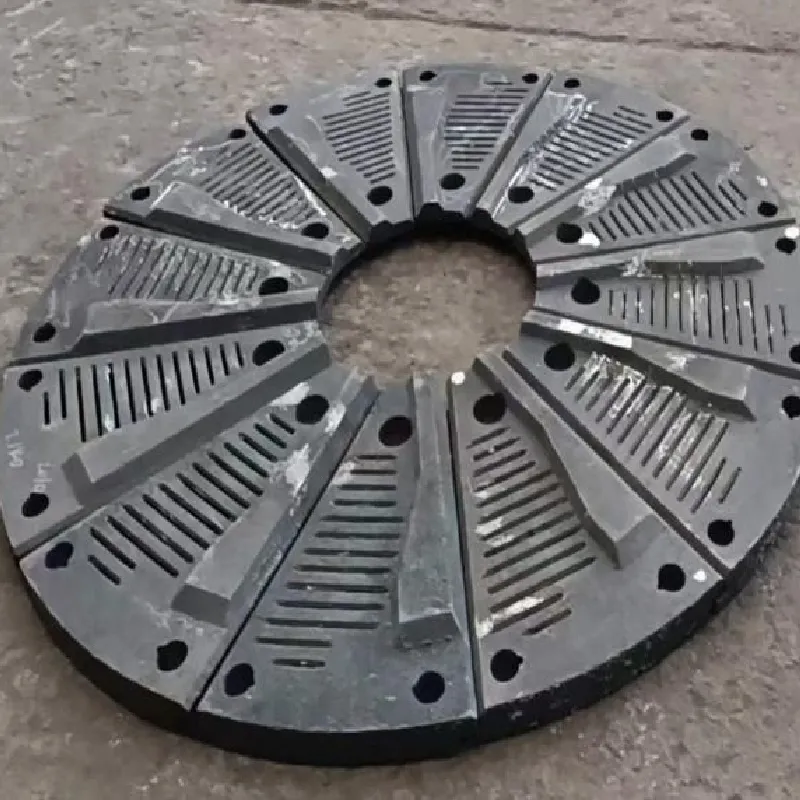
Use cases: transfer chutes, clinker coolers, cement mill inlets, crusher feed liners, cyclone bodies, fan housings, and yes—where a chromium carbide liner overlay plate might normally go but casting geometry is better.
Vendor snapshot (quick, practical view)
| Vendor | Hardness | Lead time | Certs | Notes |
|---|---|---|---|---|
| Local fabricator (AR) | HB 360–500 | ≈ 1–2 weeks | Varies | Lowest cost, shortest life. |
| Overlay plate supplier (chromium carbide liner) | HRC 55–62 | ≈ 3–5 weeks | ISO 9001 (typ.) | Great sliding abrasion; watch for delamination in impact. |
| Chengda (Hebei, CN) | HRC 60–64 | ≈ 3–6 weeks | ISO 9001:2015 | Cast geometry; robust under impact; real-world use may vary. |
Customization
Holes, countersinks, studs, beveled edges, matched segments for large radius bends, bimetal backing for weldability, and pattern kits for fast swaps. To be honest, I like their habit of sending hardness maps with the delivery—simple, transparent.
Two quick case stories
Cement plant, North Asia: AR450 chute liners were lasting ~3 months on clinker. Chengda high-chrome swap ran 11 months; ASTM G65 lab data showed 0.12 g loss (Proc A). Operators said dust abrasion “felt lower,” which matches the numbers.
Iron ore transfer, Australia: Overlay-style chromium carbide liner was chipping near impact zone. Cast high-chrome with thicker nose (25→40 mm) survived a season; downtime dropped by around 38% year over year.
Final thought
Overlay plate has its place; casting has its edge where impact and shape complexity matter. Actually, many customers say the quiet win is consistency—spec in a good casting, and you stop talking about it for a while. That’s usually the goal.
Authoritative citations
- ASTM A532/A532M – Standard Specification for Abrasion-Resistant Cast Irons. https://www.astm.org/a0532_a0532m-10r19.html
- ASTM G65 – Standard Test Method for Measuring Abrasion Using the Dry Sand/Rubber Wheel Apparatus. https://www.astm.org/g0065-16.html
- ISO 6508-1:2016 – Metallic materials — Rockwell hardness test. https://www.iso.org/standard/64071.html
- ASM Handbook, Vol. 1: Properties and Selection: Irons, Steels, and High-Performance Alloys. ASM International.
-
Optimize Industrial Milling with High Quality мелющие тела
NewsJul.01,2026
-
High Performance шлифовальные шары для добычи полезных ископаемых
NewsJun.29,2026
-
Industrial Efficiency Guide for выбор размера мелющих шаров
NewsJun.27,2026
-
High Performance шары мелющих тел из кованой стали Grinding Balls
NewsJun.26,2026
-
High Efficiency Industrial кованые мелющие тела Grinding Media
NewsJun.25,2026
-
Guide to Manganese Alloy Steel Properties and Applications
NewsJun.23,2026